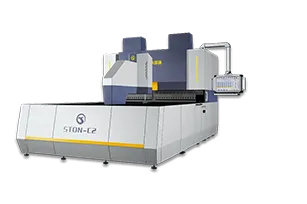
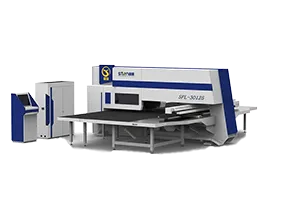
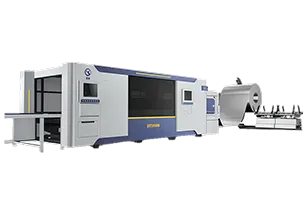
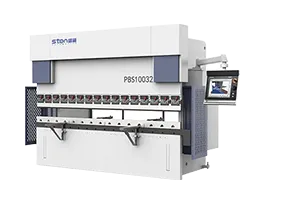
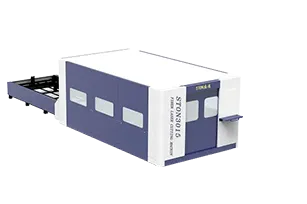
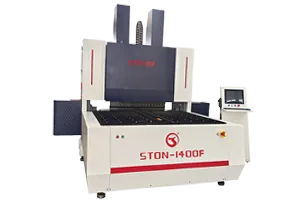
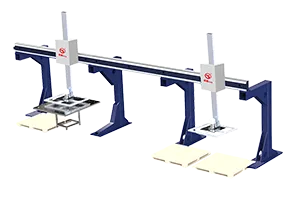
نحن مسؤولون عن البناء-----نحن مسؤولون عن التصنيع-----نحن مسؤولون عن التدريب
هل تبحث عن شريك معدات صناعية موثوق به؟
حلول ثني مصممة خصيصًا لإنتاج الصفائح المعدنية الخاصة بك - دقة عالية، وسرعة تسليم، ودعم فني كامل.
راسلنا عبر البريد الإلكتروني
تواصل معنا

    يُرجى الانتظار ريثما يتم تقديم النموذج....

    Coil-to-Part Turnkey Line — Uncoiling to Finished Bent Part

    One control system from the coil to the stack: uncoiling, levelling, laser blanking, punching, bending and palletising, with no manual handling in between.

    0.5–2.0 mmMaterial thickness window
    ≤10 TMaximum coil weight
    ±1 mm/m²Levelling accuracy
    0–12 m/minAdjustable line speed

    What is a coil-to-part line and when is it worth it?

    A coil-to-part line takes steel in coil form and returns a finished, formed, stacked component without a person touching the material in between. The chain is uncoiling → levelling → laser blanking or turret punching → automatic bending → stacking, optionally with a robot welding station at the end. Everything runs under one control system with process interlock and data traceability.

    It is worth it when three conditions hold together: your product range is reasonably standardised, your volume is continuous rather than campaign-based, and your material sits in the 0.5 to 2.0 mm window. Coil is cheaper per tonne than cut sheet, intelligent nesting from a continuous strip raises material utilisation, and the handling, shearing and work-in-progress between machines disappears. If your mix is high and your batches are small, a punch-and-bend cell fed from sheet is usually the better investment — a coil line rewards repetition, and we will say so before quoting.

    STON CNC (Qingdao Ston Mechanical Technology Co., Ltd.) is a Chinese original manufacturer of CNC panel benders and turret punch presses, founded in 2006 in Qingdao, China. All equipment described here is built inside STON CNC's own 20,000㎡ factory, from casting and heat treatment through machining, assembly and inspection. Machines carry ISO 9001 quality certification and CE marking under Machinery Directive 2006/42/EC, and are exported to more than 80 countries. View certifications and patents →

    What the line produces

    Standardised panel families, made continuously

    Coil-fed lines suit products built from a limited number of panel types repeated at high volume. Below are the part families we most often configure a line around.

    Cabinet doors and side panelsElectrical and control enclosures
    Locker and drawer bodies0.5–1.0 mm, very high repetition
    Appliance and chassis panelsStandardised, continuous demand
    Ceiling and cladding panelsLong runs, consistent section
    Ventilation and purification panelsLouvres and perforation in line
    Shelving and tray panelsRibbed, repetitive, high volume
    Door leaves and skinsFlat faces, flatness critical
    Rack and enclosure panelsPerforation plus four-sided flange
    What a coil line actually removes

    Three costs that disappear between the coil and the stack

    01

    The sheet premium and the shearing scrap

    Cut sheet carries a conversion cost per tonne over coil, and every shear operation creates offcut that a continuous strip does not. Combined with intelligent nesting across the strip, material utilisation is where a coil line usually recovers its cost first — and on thin gauge, material is the largest single item in the part cost.

    02

    Work in progress between every machine

    Sheet-based production stacks material at each stage: after shearing, after cutting, after punching, before bending. Each stack is floor space, handling labour, damage risk and cash tied up. Under one control system with process interlock, the part moves from stage to stage without ever being set down.

    03

    Flatness problems that appear at the bend

    Coil set and edge wave do not announce themselves until a panel refuses to bend straight or a door face shows a ripple. A precision leveller with 40Cr rollers on self-aligning bearings delivers a flatness of roughly ±1 mm/m² and diagonal accuracy within 1 mm over 2000 mm, so the blank arriving at the bender is already correct.

    Recommended configuration

    Three line scopes, by how far you want the automation to reach

    Lines are modular. Most customers start at the blanking end, where the material saving is, and extend to forming once the blank supply is stable.

    Coil to blank

    Uncoiling, levelling and laser blanking
    • Uncoiler and precision leveller, coil ≤10 T
    • Fiber laser blanking, 1–6 kW, multiple power options
    • Levelling accuracy ±1 mm/m²
    • Blanks feed your existing punching and bending
    • Optional dual-head cutting and dual uncoiling
    Most common scope

    Coil to formed part

    Blanking, punching, bending and stacking
    • Everything in coil-to-blank, plus:
    • CNC turret punching with automatic loading and unloading
    • Automatic panel bending with angle compensation
    • Automatic sheet separation, positioning and stacking
    • Unified control system, process interlock, data traceability
    • Rapid program switching between product variants

    Coil to welded assembly

    Adding robot welding at the end of the line
    • Everything in coil-to-formed-part, plus:
    • Welding robot, positioner, fixtures and seam tracking
    • Butt, fillet and spot welding under one schedule
    • Reduced welding distortion and manual intervention
    • Fully customised layout to your building and process flow
    • Intelligent scheduling across the whole line
    Plan against these numbers

    Line specification, utilities and footprint

    These are the figures your building, your electrical contractor and your material buyer need before a layout can be drawn. Bring them to the first engineering call.

    المعلمةValueNotes
    Raw materialCold-rolled sheet, galvanised sheet, stainless steelAluminium on request
    سماكة الصفيحة0.5–2.0 mmStainless typically ≤1.5 mm
    عرض الملف200–1500 mm (laser line typically 1000–1500 mm)Confirm against your product range
    Coil weight≤10 TDetermines uncoiler and floor loading
    Coil inner diameterφ470–630 mmConfiguration dependent
    Coil outer diameterφ1000–1600 mm—
    Levelling accuracy±1 mm/m²Decides whether flat faces stay flat
    Diagonal accuracy≤1 mm / 2000 mm—
    Threading speed5 m/minCoil changeover
    Line speed0–12 m/min, adjustableLeveller linear speed
    Running height+800 mmAffects pit and platform design
    Surface qualityFlat strip, no processing defects introduced—
    مزود الطاقة3φ AC 400 V ±5%, 50 Hz ±2%Configured to destination
    Laser 3 kW capacity≤50 kVA installed, 60 kVA supply recommended—
    Laser 6 kW capacity≤100 kVA installed, 120 kVA supply recommended—
    Compressed air0.5–0.6 MPa, 0.6 m³/min—

    Right fit

    Standardised panel families in 0.5–2.0 mm, produced continuously, where material cost dominates the part cost and the same sections repeat month after month.

    Wrong fit

    High-mix job-shop work with small batches, thickness above 2.0 mm, panels wider than the coil range, and any product built mainly from roll-formed profiles or deep-drawn shells.

    Keep a press brake

    Even with a full line, keep a press brake for specials, prototypes, thick parts and anything outside the coil width. The line handles the repeatable volume; the brake handles everything else.

    Standards this equipment is built and guarded to

    Risk assessment follows EN ISO 12100; safety-related control functions such as light-curtain interruption and emergency stop are specified to EN ISO 13849-1. Hydraulic press brakes supplied into the EU are built against EN 12622. Machines placed on the EU market carry CE marking under Machinery Directive 2006/42/EC with the accompanying technical file. Quality management is certified to ISO 9001, and machined structural tolerances follow ISO 2768. A line is a single assembly of machinery under the Machinery Directive, so risk assessment to EN ISO 12100 is carried out across the whole line rather than machine by machine, with interlocked guarding and safety functions specified to EN ISO 13849-1. Machined structural tolerances follow ISO 2768.

    On the machines this means fully enclosed rear fencing, protective covers on all protruding moving parts, laser guarding that halts motion when the protected zone is broken, over-tonnage protection on turret punch presses, and grating-ruler offset-load detection on panel benders.

    Choosing the process

    Coil-fed line, sheet-fed cell or outsourced blanking?

    The right answer depends almost entirely on how repetitive your product range is. A coil line rewards repetition and punishes variety.

     Coil-to-part lineSheet-fed punch and bend cellOutsourced blanking
    Best forStandardised ranges, continuous volumeMixed ranges, medium batchesLow volume or unstable demand
    Material cost per partLowest — coil price plus nestingSheet price, nesting within the sheetHighest — includes supplier margin
    Handling between stagesNone — continuousStacked and moved between machinesTransport, inspection, storage
    Work in progressMinimalModerateHigh — buffer stock required
    Response to a design changeProgram change, coil width permittingProgram changeSupplier lead time
    Floor spaceLargest footprintModerateSmallest
    Capital requiredHighestModerateLowest
    Suits thickness above 2 mmلاBending limited, punching capableSupplier dependent
    Does STON supply it?YesYesNot applicable

    If your range changes frequently or your volume arrives in campaigns rather than continuously, we will recommend a sheet-fed cell instead. A coil line bought for a variable product mix spends its life waiting for coil changeovers, which is the most expensive way to be idle.

    Process flow

    Six stages under one control system

    1. UncoilingContinuous unwinding, synchronised with the leveller▶
    2. Levelling40Cr rollers, self-aligning bearings, ±1 mm/m²▶
    3. Laser blankingFiber laser with nesting, burr-free edge▶
    4. PunchingHoles, louvres, ribs, forming, automatic handling▶
    5. BendingAngle compensation, program switching, stacking▶
    6. WeldingOptional robot station with seam tracking
    What changes

    Sheet-based production versus a coil-fed line

    Figures below describe the direction and mechanism of the change. Actual results depend on your part mix, batch size and shift pattern — we model them against your own drawings before quoting.

    ItemSheet, standalone machinesCoil-to-part line
    Material input costCut sheet, conversion premium per tonneCoil, lowest cost per tonne
    Material utilisationNesting limited by sheet sizeNesting across a continuous strip
    Handling operationsStack and move at every stageNone between stages
    Work in progressBuffers at each machineMinimal, process interlocked
    Blank flatness at the benderCoil set and edge wave carried throughLevelled to ±1 mm/m² before cutting
    Secondary positioningRe-clamped at each machineOne reference through the line
    LabourOperators at each machineLine supervision, not machine tending
    TraceabilityPer machine, manually linkedUnified control, data traceability across the line
    Flexibility on new productsHighCoil width and thickness constrained

    Payback logic we use with customers: (annual labour released + reduction in rework and scrap + additional saleable output) ÷ installed equipment cost. We build this with your real numbers rather than publishing a headline figure that would not match your plant.

    المعدات المستخدمة في هذا الحل

    The modules that make up the line

    STON uncoiling levelling and fiber laser cutting production line
    Blanking

    فك اللفائف والتسوية والقطع بالليزر

    Welded and heat-aged uncoiler body, precision leveller with 40Cr rollers on self-aligning or needle bearings, fiber laser with process parameter database and AutoCAD-compatible programming, dual-temperature water cooling.

    View the blanking line →
    STON automatic laser bending production line for coil fed sheet metal
    Full line

    خط الثني الأوتوماتيكي بالليزر

    The complete chain from coil to formed part under one control system, with process interconnection, intelligent scheduling and data traceability. Layout planned around your product structure, capacity and building.

    View the full line →
    STON SF series servo CNC turret punch press integrated into a production line
    Punching

    مكبس الثقب البرجي CNC بالسيرفو

    Punching, trimming, forming, louvring and rib pressing with automatic loading, sheet separation, positioning, unloading and stacking. ±0.1 mm accuracy, turret speed to 40 rpm.

    View SF series →
    STON CNC panel bender integrated with automatic loading in a production line
    Forming

    ماكينة ثني الألواح CNC مع التحميل الآلي

    Integrated feeding, positioning, bending and unloading with angle compensation and rapid program switching. Models to 2800 mm forming length, cast or welded frames, native automation interface.

    View press arm type →
    STON truss loading and unloading system linking line stages
    Handling

    معالجة الجمالون والروبوت

    Links the stages so material is never set down. Compatible with most robotic arm and gantry brands, with vacuum pick-up that protects coated and filmed surfaces through the whole line.

    View truss system →
    STON double platform fiber laser cutting machine used alongside a coil line
    Alongside

    قطع بالليزر بمنصة مزدوجة

    For the parts that fall outside the coil width or run in short batches. Most coil-line customers keep a sheet laser alongside so the line is never stopped for a special.

    View laser unit →
    لماذا STON

    An original manufacturer, from casting to commissioning

    Founded in 2006 and headquartered in Qingdao, one hour from major export ports and the airport. Casting, heat treatment, machining, welding, assembly and inspection all happen inside our own 20,000㎡ factory. That is why a configuration change for a full production line does not become a six-month subcontracting problem.

    STON CNC 20,000 square metre manufacturing facility in Qingdao
    20,000㎡ facility, 300+ processing machines
    CNC gantry milling and boring centres machining large machine frames
    Gantry milling for long line components
    Automated welding and machining processes at the STON factory
    Full automation in welding and machining
    Customers visiting the STON CNC factory for line acceptance
    Customer factory tours and line acceptance
    Tour the factory Open the 360° virtual tour
    After the machine lands

    Support that stays with the line

    A line is a project, not a purchase. Layout, factory acceptance testing, shipping, installation, commissioning, training and handover are all part of the scope, and all of them are handled by STON's own engineers.

    1-hour response, 48-hour on siteGlobal service coverage across 80+ export countries.
    Free sample parts before you orderPre-sales engineers review drawings and validate feasibility, tooling and bend programs.
    Lifetime machine trackingUnique machine ID, free software upgrades, quarterly inspection and maintenance advice.
    7×24 expert technical supportRemote diagnostics plus on-site engineers when required.
    Operator and programmer trainingVideo tutorials, manuals and on-site sessions during commissioning.
    Dedicated spare parts inventoryConsumables and wear parts held for fast dispatch.
    VX
    Vicky Xu Head of Overseas Sales, STON CNC

    Ten years working with sheet-metal manufacturers across Europe, Southeast Asia, the Middle East and South America. Rather than quoting a machine from a catalogue, Vicky starts from your part drawings, material and thickness range and target output, then works with STON's engineering team to define the configuration — a single panel bender, a turret punch press, or a fully integrated cutting, punching and bending line with automated loading.

    Questions we get about coil-fed lines

    Frequently asked questions

    ما كمية المواد التي نوفرها بالفعل من خلال التحول من الصفائح إلى اللفائف؟
    يجتمع هنا تأثيران. فتكلفة الكويل لكل طن أقل من تكلفة الصفائح المقطوعة لأنك لا تدفع مقابل عملية التحويل، كما أن التعشيق (nesting) على طول شريط متواصل أقل تقييدًا من التعشيق داخل مقاس صفيحة ثابت، وبالتالي تقل نسبة الخردة الناتجة. ويعتمد حجم الوفورات على هندسة القطعة ومستوى كفاءة التعشيق الحالي لديك، ولهذا السبب نقوم بنمذجته بالاستناد إلى قطعك الفعلية بدلاً من تقديم نسبة عامة. وفي حالة السماكات الرقيقة، حيث تمثل المادة الخام أكبر عنصر منفرد في تكلفة القطعة، غالبًا ما يكون هذا هو المجال الذي يستعيد فيه الخط استثماره أولاً.
    تتغير تشكيلة منتجاتنا باستمرار. فهل لا يزال خط إنتاج الملفات هو الخيار المناسب؟
    على الأرجح لا، وسنقول ذلك صراحةً. فخط الإنتاج الذي يعمل باللفائف يناسب عمليات التصنيع المتكررة. أما إذا كانت دفعاتك صغيرة ومجموعة منتجاتك متنوعة، فسيقضي الخط وقته في عمليات تبديل اللفائف، في حين أن وحدة التثقيب والانحناء التي تعمل بتغذية الألواح ستوفر لك عائدًا أفضل برأسمال أقل ومساحة أرضية أقل. والاختبار الحقيقي هو ما إذا كانت مجموعة صغيرة من عائلات الألواح تمثل معظم حجم الإنتاج لديك.
    ماذا لو قمنا بتصنيع عدة سماكات وعروض مختلفة؟
    يكلف كل تغيير للملف وقتًا في عملية التثبيت بمعدل 5 م/دقيقة بالإضافة إلى وقت الإعداد. يمكن تهيئة خط الإنتاج باستخدام نظام فك لف مزدوج لتقليل ذلك، كما يمكن التبديل بين برامج المنتجات بسرعة، لكن الاعتبارات الاقتصادية الأساسية لا تزال تفضل نطاقًا ضيقًا من السماكات والعروض. أحضر قائمة المواد الفعلية الخاصة بك إلى أول اجتماع هندسي — فغالبًا ما تؤدي هذه القائمة إلى تغيير النطاق الموصى به أكثر مما يؤديه رقم الحجم.
    ما هي المساحة الأرضية المطلوبة وما هو نوع الأساس الذي يحتاجه خط الإنتاج؟
    تعتمد المساحة المطلوبة على نطاق العمل وحجم الليزر؛ ويبلغ الارتفاع التشغيلي +800 مم، ويتم رسم المخططات وفقًا لمبناك الخاص بدلاً من استخدام قالب قياسي. ويحدد وزن اللفائف الذي يصل إلى 10 أطنان الحمل الأرضي عند جهاز فك اللفائف. أرسل مخططًا لمبناك يتضمن مواقع الأعمدة وارتفاعات الأبواب ونطاق تغطية الرافعات، وسنرسل إليك رسمًا تخطيطيًّا محددًا فيه مواقع المرافق.
    ما هي احتياجات الخط من الطاقة والهواء المضغوط؟
    مصدر الطاقة هو تيار متردد ثلاثي الأطوار (3φ) بجهد 400 فولت ±5%، وتردد 50 هرتز ±2%. ويبلغ ضغط الهواء المضغوط 0.5–0.6 ميجا باسكال بمعدل تدفق 0.6 متر مكعب/دقيقة. بالنسبة للليزر، تبلغ السعة المركبة لوحدة 3 كيلوواط ≤50 كيلوفولت أمبير مع توصية بتزويدها بـ 60 كيلوفولت أمبير، وتبلغ السعة المركبة لوحدة 6 كيلوواط ≤100 كيلوفولت أمبير مع توصية بتزويدها بـ 120 كيلوفولت أمبير. يتم ضبط الجهد والتردد وفقًا لبلد الوجهة قبل الشحن.
    كم تبلغ تكلفة خط الإنتاج من الملف إلى القطعة؟
    Line pricing is scope-driven and varies more than any single machine. The main factors are: laser power (1 kW to 6 kW, with 3 kW and 6 kW most common), coil handling capacity and whether dual uncoiling is fitted, which stages are included (blanking only, blanking plus forming, or with robot welding), the level of automatic handling and stacking, و the degree of customisation to your building and process flow. A coil-to-blank scope and a full coil-to-welded-assembly line differ by a wide margin. Send your product drawings, volume and building plan and we return a scoped proposal with the alternatives priced alongside.
    كم من الوقت يستغرق مشروع خط الإنتاج بدءًا من الطلب وحتى مرحلة الإنتاج؟
    تتضمن مراحل المشروع ما يلي: الموافقة على المخطط، والتصنيع، واختبار القبول في المصنع لدى شركة STON، والشحن، والتركيب، والتشغيل التجريبي، وتدريب المشغلين، والتسليم. ونظرًا لأن كل مرحلة يتم تنفيذها داخليًّا، فإن مخاطر الجدول الزمني تتركز في مرحلة الشحن وجاهزية موقعكم الخاص، وليس في المقاولين من الباطن. ويتم إصدار الجدول الزمني للمشروع مع مخطط التصميم.
    هل يمكن دمج خط إنتاج في مصنع قيد التشغيل بالفعل؟
    نعم، وهذه هي الحالة الأكثر شيوعًا. تتميز خطوط الإنتاج بطابعها المعياري، لذا يمكن تنفيذ التركيب على مراحل — عادةً ما تبدأ بعمليات القطع أولاً، ثم التشكيل — بحيث يستمر الإنتاج الحالي. ويتم تحديد واجهات التوصيل مع المعدات التي تمتلكها بالفعل في مرحلة التصميم.
    هل تحمل المجموعة بأكملها علامة CE؟
    يُعتبر خط الإنتاج مجموعة واحدة من الآلات بموجب توجيه الآلات 2006/42/EC، لذا فإن تقييم المخاطر وفقًا للمعيار EN ISO 12100 يشمل الخط ككل وليس آلةً آلةً، مع وجود حواجز أمان مترابطة ووظائف تحكم متعلقة بالسلامة وفقًا للمعيار EN ISO 13849-1. يتم إعداد الوثائق الفنية مع كل شحنة متجهة إلى الاتحاد الأوروبي.
    هل يمكن توريد هذه الخطوط إلى تركيا أو المكسيك أو روسيا أو جنوب شرق آسيا؟
    نعم — هذه هي بعض من الأسواق التصديرية الرئيسية لشركة STON CNC. يتم ضبط جهد التيار والتردد وفقًا لمتطلبات الوجهة قبل الشحن، ويمكن ترجمة لغة نظام التحكم الرقمي (CNC) وواجهة المستخدم (HMI) إلى اللغة المحلية، كما يمكن تحديد العلامة التجارية لنظام التحكم إذا كانت شبكة الخدمة المحلية تدعم علامة تجارية معينة بالفعل. تتم عمليات التعبئة وتحميل الحاويات لخط الإنتاج الكامل داخليًّا في تشينغداو، التي تبعد ساعة واحدة عن الموانئ الرئيسية للتصدير.
    كيف يتم التعامل مع قطع الغيار والخدمات لخط إنتاج كامل؟
    تلتزم شركة STON CNC بالاستجابة في غضون ساعة واحدة وحل المشكلات في الموقع خلال 48 ساعة في جميع أسواق التصدير التي تزيد عن 80 سوقًا، مع توفير دعم فني عن بُعد على مدار 7×24 وتحديثات برمجية مجانية طوال عمر المعدات. بالنسبة للخط الإنتاجي، نقدم عرض أسعار لمجموعة قطع غيار موصى بها تغطي قطع التآكل في كل مرحلة، لأن فقدان أحد المستهلكات في وحدة واحدة يؤدي إلى توقف الخط بأكمله وليس آلة واحدة فقط.
    كيف يمكننا معرفة ما إذا كان خط ما مناسبًا لنا قبل الالتزام به؟
    يرجى إرسال رسومات منتجاتكم، وحجم الإنتاج الشهري حسب فئة القطع، وقائمة المواد، ومخطط مبنى شركتكم. وسيقوم مهندسونا بتقديم توصية محددة النطاق — والتي قد تكون عبارة عن خلية تعمل بتغذية الألواح بدلاً من خط الإنتاج — إلى جانب عينات مجانية من القطع للتحقق من الجدوى قبل تقديم أي طلب شراء.

    Specifications on this page verified against STON engineering documentation on 4 August 2026. Forming limits are confirmed against your own drawings before quotation. Published on 4 August 2026 · Last updated 4 August 2026 · Reviewed by Vicky Xu, Head of Overseas Sales.

    Next step

    Send us your product range and building plan

    A line is designed around your parts and your floor, not the other way round. Send the drawings and a building plan and we return a scoped layout, a utility list and an honest view on whether a coil line or a sheet-fed cell suits you better.

    • Feasibility review by pre-sales engineers, not a sales rep
    • Free sample parts before you place an order
    • Line layout drawn against your actual floor plan
    • Configuration options at three output levels

    Prefer to talk first?
    WhatsApp: +86 18153226091
    البريد الإلكتروني: [email protected]

    احصل على اقتراح للتجهيز

    Send your requirements through our secure enquiry form. Our team will reply within 24 hours.

      احصل على اقتراح للتجهيز

      نرد خلال 24 ساعة. تُعامل رسوماتك بسرية تامة.

      يمكن إرفاق الرسومات في رسالة الرد الإلكترونية. نرد خلال 24 ساعة من الاثنين إلى السبت.

      يُرجى الانتظار ريثما يتم تقديم النموذج....

      احصل على عرض أسعار الآن

      أرسل لنا احتياجاتك - سنعاود الاتصال بك خلال 24 ساعة

      سواء أكنت تقوم بترقية خط إنتاج قائم أو تبدأ مشروعًا جديدًا، فإن STON ستخصص حلاً بنظام التحكم الرقمي للإنتاج الخاص بك.