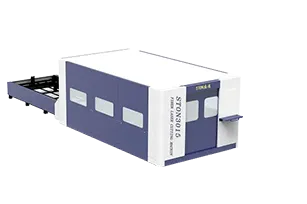
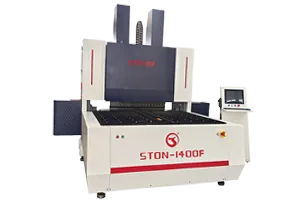
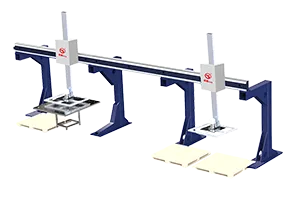
نحن مسؤولون عن البناء-----نحن مسؤولون عن التصنيع-----نحن مسؤولون عن التدريب
هل تبحث عن شريك معدات صناعية موثوق به؟
حلول ثني مصممة خصيصًا لإنتاج الصفائح المعدنية الخاصة بك - دقة عالية، وسرعة تسليم، ودعم فني كامل.
راسلنا عبر البريد الإلكتروني
تواصل معنا

    يُرجى الانتظار ريثما يتم تقديم النموذج....

    الثني الآلي لمصنعي خزائن الملفات وخزائن التخزين والأثاث المعدني

    Drawer fronts, door leaves and locker wraps in 0.5–1.0 mm pre-painted sheet — formed without a single manual lift, and without a scratch on the visible face.

    0.5 mmThinnest sheet formed reliably
    360°Patented rotating vacuum feeding
    5 ملمالارتفاع الأدنى للانحناء
    48 ساعةالاستجابة العالمية في الموقع

    What equipment does a filing cabinet or locker factory actually need?

    Metal furniture is the highest-volume, thinnest-gauge corner of sheet metal. A locker or filing cabinet is built from a small number of part types — drawer fronts, drawer boxes, door leaves, shelf panels, body wraps — each repeated thousands of times a month in 0.5 to 1.0 mm pre-painted or galvanised sheet. Because the part count per cabinet is low and the volume per part is enormous, the economics are decided by two things only: seconds per part و scrap caused by handling damage.

    That points at a specific machine set. Blanks come from a coil-fed line or a ليزر الألياف. Forming is done on a ثني الألواح باستخدام الحاسب الآلي الرقمي with vacuum pick-up, or on a flexible edge folding machine where the part needs dead edges, offsets or arc bends. Loading and unloading is automated from the start, not added later — on 0.6 mm painted sheet, every manual handling step is a scrap risk. A press brake stays for brackets and hardware mounts only.

    شركة STON CNC (شركة تشينغداو شينغتونغ للتكنولوجيا الميكانيكية المحدودة) هي شركة صينية متخصصة في تصنيع آلات ثني الألواح بالتحكم الرقمي (CNC) وآلات الثقب ذات البرج، وقد تأسست عام 2006 في مدينة تشينغداو، الصين. يتم تصنيع جميع المعدات المذكورة هنا داخل مصنع شركة STON CNC الذي تبلغ مساحته 20,000 متر مربع، بدءًا من عملية الصب والمعالجة الحرارية وصولاً إلى التصنيع الآلي والتجميع والفحص. تحمل الآلات شهادة الجودة ISO 9001 وعلامة CE بموجب توجيه الآلات 2006/42/EC، ويتم تصديرها إلى أكثر من 80 دولة. عرض الشهادات وبراءات الاختراع →

    الأجزاء التي نصنعها من أجل

    The same six parts, ten thousand times a month

    Metal furniture production is the opposite of job-shop work: very few part types, very high repetition, very thin material, and a visible painted face that cannot be marked. That combination is exactly where automated panel bending pays back fastest.

    Drawer fronts0.6–0.8 mm, visible face, tight flatness
    Drawer boxesFour-sided forming, hemmed edges
    Door leavesUp to 2000 × 1500 mm, no waves
    Locker body wrapsLong single-piece wrap-around bends
    Shelf panelsRibbed for load, high repetition
    Back panels0.5 mm, thinnest part in the cabinet
    Top and base platesCut-outs plus four-sided flange
    Plinth and toe sectionsSmall parts, very high volume
    Where metal furniture production leaks margin

    Three problems every locker factory recognises

    01

    Thin painted sheet marks at every touch

    A 0.6 mm pre-painted drawer front picks up a scratch from a glove, a bench edge or a back gauge. Rework means stripping and repainting, which costs more than the part. Vacuum pick-up with a patented 360° rotating suction feeder moves the blank without touching the visible face at all.

    02

    Thin gauge fights back

    Below 0.8 mm, springback and edge waviness turn into visible defects on a flat door face. Closed-loop servo bending with rapid compensation adjustment holds the angle across the full length instead of relying on an operator to shim and retry.

    03

    Volume turns seconds into money

    When one part runs 20,000 times a month, two seconds of cycle time is a shift per month. Press-brake pacing is operator-limited; a panel bender folds all four sides from one clamping, and with automatic loading it keeps running through breaks and shift changes.

    الإعدادات الموصى بها

    Three ways to build the cell, by monthly volume

    Metal furniture is the one industry where we push customers towards automation earlier than they expect. At locker volumes, a manual-load machine becomes the bottleneck within a year.

    خلية الإدخال

    Moving off press brakes, up to ~5,000 parts/month
    • Suction cup panel bender, A (1000) or B (1400)
    • Welded frame, CRS ≤1.5 mm / SS ≤1.0 mm
    • Manual loading, one operator
    • Custom pressure and folding knives for drawer profiles
    • Footprint from 4.3 × 1.6 m
    Most furniture factories

    Standard cell

    Mixed locker and cabinet ranges, 5,000–30,000 parts/month
    • Panel bender B+ (1600) or C (2000), cast-iron frame
    • Flexible edge folding machine for dead edges and offsets
    • Truss or robotic loading with vacuum grippers
    • Automatic stacking, no operator contact with the painted face
    • Auxiliary upper and lower blades for local small bends
    • Automatic tool change for switching between drawer sizes

    Coil-fed line

    Standardised ranges, continuous output
    • Uncoiling and levelling, coil ≤10 T, 200–1500 mm wide
    • Levelling accuracy ±1 mm/m² for flat door faces
    • Fiber laser or turret punch blanking
    • Panel bending with automatic stacking
    • Optional robot welding station for drawer boxes
    • التحكم الموحد، الترابط بين العمليات، إمكانية تتبع البيانات
    قبل أن تواصل القراءة

    ما يمكن لهذه الآلات تشكيله وما لا يمكنها تشكيله

    Metal furniture sits comfortably inside the forming window — the risk here is not thickness, it is part size at the small end. Drawer components and plinth sections often sit close to the minimum forming dimension, which is the first thing our engineers check on your drawings.

    المعلمةآلة ثني الألواحآلة طي الحواف المرنةملاحظات
    Typical furniture gauge0.5–1.0 mm0.5–1.0 mmأقل بكثير من السعة الاستيعابية
    Cold-rolled steel max≤1.5 mm welded / ≤2.0 mm cast—عند طول الانحناء الكامل
    الفولاذ المقاوم للصدأ (الحد الأقصى)≤1.0 mm welded / ≤1.2 mm cast—For stainless furniture ranges
    الحجم الأقصى للتشكيل1000 × 1000 to 2800 × 1500 mm1200 × 1200 إلى 2000 × 1500 ملمحسب الطراز
    الحجم الداخلي الأدنى ذو الأربعة جوانبحوالي 140 × 190 ملم200 × 200 ملمCheck small drawer parts here
    الارتفاع الأدنى للانحناء5 ملم4 ملمBelow this, press brake or custom tooling
    Max bending height170 / 300 / 400 ملم100 ملمBy configuration
    العمليات الخاصةPositive and negative bending, 0–180°القوس، الحافة الميتة، الإزاحةHemmed drawer edges use dead edge
    دقة الزاويةapprox. ±0.5°/mapprox. ±0.5°/mStraightness approx. 0.2 mm/m
    المرافق العامةثلاثي الأطوار، 380 فولت، هواء مضغوط بضغط 0.6 ميجا باسكالتم ضبطه على الجهد المطلوب

    المقاس المناسب

    Four-sided folded panels in 0.5–1.0 mm repeated at high volume, with a visible painted or coated face that must stay unmarked. This is the strongest case for automated panel bending anywhere in sheet metal.

    مقاس غير مناسب

    Roll-formed shelving uprights and rack posts, deep-drawn parts, wire products, and any drawer component whose four-sided inner size falls below the minimum forming dimension.

    احتفظ بمكبس ثني

    Hardware mounts, lock reinforcement plates, hinge brackets and prototype runs. One press brake alongside an automated cell covers everything the bender should not be set up for.

    المعايير التي صُنعت هذه المعدات وفقًا لها وتلتزم بها

    فيما يلي تقييم المخاطر EN ISO 12100؛ وقد تم تحديد وظائف التحكم المتعلقة بالسلامة، مثل انقطاع ستارة الضوء والإيقاف في حالات الطوارئ، بحيث EN ISO 13849-1. يتم تصنيع مكابس الثني الهيدروليكية التي يتم توريدها إلى الاتحاد الأوروبي وفقًا لـ EN 12622. تحمل الأجهزة المعروضة في سوق الاتحاد الأوروبي علامة CE بموجب توجيه الآلات رقم 2006/42/EC مع الملف الفني المرفق. وقد حصلت إدارة الجودة على شهادة ISO 9001، وفيما يلي التفاوتات الهيكلية الناتجة عن المعالجة الآلية ISO 2768. For the finished furniture, most export markets reference EN 16121 for non-domestic storage furniture (strength, durability and stability) — the forming tolerances and joint consistency your product needs to pass it are set at the bending stage.

    وبالنسبة للآلات، يعني ذلك وجود سياج خلفي مغلق تمامًا، وأغطية واقية على جميع الأجزاء المتحركة البارزة، وأنظمة حماية بالليزر تعمل على إيقاف الحركة عند اختراق المنطقة المحمية، ونظام حماية من الحمولة الزائدة في مكابس الثقب ذات البرج الدوار، ونظام كشف الحمل المنحرف باستخدام شبكة قياس في آلات ثني الألواح.

    اختيار العملية

    Panel bender, folding machine or press brake?

    Metal furniture factories usually need two of these three. The split is decided by whether the part needs a hemmed or arc edge, and by how small the part is.

     ثني الألواح باستخدام الحاسب الآلي الرقميآلة طي الحواف المرنةمكبس الكبح CNC
    Best forFour-sided boxes and drawersPanels needing dead edge, arc or offsetBrackets, hardware, prototypes
    Typical furniture partsDrawer boxes, door leaves, body wrapsHemmed drawer fronts, curved shelf edgesLock plates, hinge mounts
    Max bending height170 / 300 / 400 ملم100 ملمTool-dependent
    الحجم الداخلي الأدنى ذو الأربعة جوانبحوالي 140 × 190 ملم200 × 200 ملمNo practical limit
    Handling of painted faceVacuum pick-up, no contactSuction feeding, no contactManual, contact at every step
    Operators1, or 0 with automatic loading1, or 0 with automatic loading1–2
    Economic batchMedium to very high volumeMedium to very high volumeOne-off to medium
    هل توفره شركة STON؟نعمنعمنعم

    If your range uses roll-formed shelving uprights or wire drawer runners, those come from a different process and a different supplier — we will tell you that at the drawing-review stage rather than after the order.

    مسار العملية

    From coil or sheet to a stacked, paint-ready panel

    1. الحجبCoil uncoiling and levelling, or fiber laser▶
    2. PunchingLock holes, vent slots, shelf slots, ribs▶
    3. LoadingVacuum pick-up, 360° rotating feeder▶
    4. الانحناءFour sides formed from one clamping▶
    5. أعمال الحوافDead edge, offset or arc on the folding machine▶
    6. التكديسAutomatic, no contact with the visible face
    ما هي التغييرات؟

    Manual bending versus an automated furniture cell

    توضح الأرقام الواردة أدناه اتجاه التغيير وآليته. وتعتمد النتائج الفعلية على تركيبة القطع وحجم الدفعة ونظام نوبات العمل — ونقوم بمحاكاتها وفقًا لرسوماتكم قبل تقديم عرض الأسعار.

    العنصرPress brakes onlyPanel bender cell with vacuum loading
    Operators at the bending station2 per machine on door leaves1, or unattended with automatic loading
    Handling per four-sided part4 lifts and rotations1 vacuum pick, machine does the rest
    Bend cycleOperator-paced0.2 s per bend, 5,000+ bends per day (STON published figures)
    Scratch and dent scrap on painted sheetRisk at every manual touchNo contact with the visible face
    Angle consistency across 10,000 partsDrifts with operator and shiftClosed-loop servo, ±0.5°/m
    Changeover between drawer sizesTool swap and gauge resetProgram recall plus rapid compensation adjustment
    Night shiftRequires full crewRuns unattended with automatic loading and stacking

    منطق حساب فترة الاسترداد الذي نستخدمه مع العملاء: (العمالة الموفرة سنويًّا + انخفاض إعادة العمل والخردة + الإنتاج الإضافي القابل للبيع) ÷ تكلفة المعدات المركبة. ونقوم بحساب ذلك بناءً على أرقامكم الفعلية، بدلاً من نشر رقم عام قد لا يتطابق مع واقع مصنعكم.

    المعدات المستخدمة في هذا الحل

    STON machines used in filing cabinet and locker production

    STON suction cup type CNC panel bender forming a thin gauge metal furniture panel
    التشكيل

    آلة ثني الألواح المزودة بكؤوس شفط

    Vacuum-gripped feeding designed for thin, coated sheet. Patented 360° rotating suction pick-up, full-electric servo closed-loop control, cast or welded frames, cabinet air conditioning for constant-temperature electrics.

    عرض النوع المزود بكوب شفط →
    STON flexible edge folding machine with automatic loading and unloading
    Edge work

    آلة طي الحواف المرنة

    Arc, dead edge and offset bending up to 2000 × 1500 mm, minimum bending height 4 mm. Up to 25 concurrent servo axes, 42CrMo forged blank holder, fully enclosed safety fencing.

    عرض آلة الطي →
    STON SF series servo CNC turret punch press for locker and cabinet panels
    اللكم

    مكبس الثقب البرجي CNC بالسيرفو

    Lock holes, ventilation slots, shelf-pitch slotting and stiffening ribs in one clamping. Brush and steel-ball composite table protects coated surfaces; ±0.1 mm accuracy, turret speed to 40 rpm.

    عرض سلسلة SF →
    STON uncoiling levelling and laser blanking line for metal furniture production
    إخفاء

    Coil-to-Part Production Line

    Uncoiling, levelling and laser blanking under one control system. Levelling accuracy ±1 mm/m² keeps 0.6 mm door faces flat, coil width 200–1500 mm, coil weight ≤10 T.

    عرض خط الإنتاج →
    STON double platform fiber laser cutting machine for furniture panel blanking
    Cutting

    قطع بالليزر بمنصة مزدوجة

    Exchange-table fiber laser so the next sheet loads while the current one cuts. Burr-free edges matter on furniture parts that are handled by end users, not just assemblers.

    عرض وحدة الليزر →
    STON truss and robotic loading unloading system for panel benders
    Automation

    الهياكل الحاملة والتحميل الآلي

    Native interface on every panel bender, compatible with most robotic arm and gantry brands. Removes the two-person lift on locker door leaves and lets the cell run through breaks.

    View truss system →
    لماذا STON

    شركة تصنيع أصلية، بدءًا من عملية الصب وحتى التشغيل

    Founded in 2006 and headquartered in Qingdao, one hour from major export ports and the airport. Casting, heat treatment, machining, welding, assembly and inspection all happen inside our own 20,000㎡ factory. That is why a configuration change for a locker or drawer line does not become a six-month subcontracting problem.

    منشأة تصنيع «ستون سي إن سي» التي تبلغ مساحتها 20,000 متر مربع في تشينغداو
    منشأة بمساحة 20,000 متر مربع، وأكثر من 300 آلة معالجة
    تجميع دقيق بدقة تبلغ ±0.05 مم في شركة STON CNC
    دقة التجميع ±0.05 مم
    Large annealing furnace used for stress relief of machine frames
    Annealing for long-term frame stability
    محطة فحص ذات ثلاثة إحداثيات في شركة STON CNC
    الفحص ثلاثي الأبعاد قبل الشحن
    جولة في المصنع افتح الجولة الافتراضية بزاوية 360 درجة
    بعد هبوط الطائرة

    دعم يتماشى مع الخط

    Furniture production runs to retail delivery windows and container bookings. A stopped bending cell stops the paint line behind it, so response time matters more than any single number on the datasheet.

    الاستجابة خلال ساعة واحدة، والتواجد في الموقع خلال 48 ساعةتغطية عالمية للخدمات تشمل أكثر من 80 دولة مصدرة.
    عينات مجانية من القطع قبل تقديم الطلبيقوم مهندسو ما قبل البيع بمراجعة الرسومات والتحقق من الجدوى وبرامج الأدوات وبرامج الثني.
    تتبع الجهاز مدى الحياةرقم تعريف فريد للآلة، وترقيات مجانية للبرامج، وفحص ربع سنوي، ونصائح بشأن الصيانة.
    دعم فني متخصص على مدار الساعة طوال أيام الأسبوعالتشخيص عن بُعد بالإضافة إلى استدعاء المهندسين إلى الموقع عند الحاجة.
    تدريب المشغلين والمبرمجيندروس فيديو، وأدلة إرشادية، وجلسات تدريبية في الموقع أثناء مرحلة التشغيل.
    مخزون مخصص لقطع الغيارالمواد الاستهلاكية وقطع الغيار المعرضة للتلف متوفرة للشحن الفوري.
    VX
    Vicky Xu رئيس قسم المبيعات الخارجية، شركة STON CNC

    عشر سنوات من العمل مع شركات تصنيع الصفائح المعدنية في أنحاء أوروبا وجنوب شرق آسيا والشرق الأوسط وأمريكا الجنوبية. بدلاً من تقديم عرض أسعار لآلة من الكتالوج، تبدأ فيكي من رسومات قطعك ونطاق المواد والسماكة والإنتاج المستهدف، ثم تعمل مع فريق الهندسة في STON لتحديد التكوين — سواء كانت آلة ثني الألواح الفردية، أو مكبس التثقيب البرجي، أو خط متكامل تمامًا للقطع والتثقيب والثني مع التحميل الآلي.

    Questions we get from metal furniture factories

    الأسئلة الشائعة

    Can a panel bender handle 0.5 mm sheet without marking or distorting it?
    Yes — thin coated sheet is one of the main reasons furniture factories move to a panel bender. The blank is picked up by vacuum and never dragged across a bench or a back gauge, and the patented 360° rotating suction feeder rotates the part in the air rather than on a surface. Closed-loop servo control with rapid compensation adjustment holds the angle on gauges where a press brake would rely on operator shimming.
    What is the smallest drawer or plinth part a panel bender can form?
    The minimum inner dimension for four-sided forming is approximately 140 × 190 mm on a panel bender, and 200 × 200 mm on a flexible edge folding machine. Minimum bending height is 5 mm and 4 mm respectively. Small plinth and toe sections frequently sit near this line — send those drawings first, because they decide whether the whole part family fits one machine or needs a small-part customisation with modified clamping and tooling.
    Can it produce hemmed or dead edges on drawer fronts?
    Yes, on a flexible edge folding machine, which performs arc bending, dead edge (hemming) and offset in addition to positive and negative bending. Many furniture factories run a panel bender for the boxes and a folding machine for the visible hemmed fronts. Which parts go where is decided during drawing review.
    How much faster is this than the press brakes we run now?
    STON publishes a bending speed of 0.2 seconds per bend, stated as three to four times faster than a press brake, with more than 5,000 bends per day per machine. For metal furniture the more important number is usually labour and scrap: a door leaf that needs two operators on a press brake is handled by one on a panel bender, or by none with automatic loading, and handling scrap on painted sheet largely disappears.
    How much does a locker and filing cabinet bending cell cost?
    There is no list price, because the cell is configured to the part family. Five factors move the figure most: frame type (welded costs less than cast iron but is limited to 1.5 mm cold-rolled rather than 2.0 mm), طول التشكيل from 1000 mm to 2800 mm, مستوى الأتمتة (manual load, truss loading or a full robotic cell with stacking), the tooling package including custom drawer knives and auxiliary blades, and نطاق — a single bender, a bender plus folding machine, or a coil-fed line. A single manual-load machine and a coil-to-part line differ by roughly an order of magnitude. Send your part drawings and monthly volume and we return a configured quotation within 24 hours, with the alternatives priced alongside.
    Panel bender, folding machine or press brake — which do we need?
    Panel bender for four-sided boxes and drawer bodies. Flexible edge folding machine for panels needing dead edges, arcs or offsets, and for very long single-piece wraps. Press brake for brackets, hardware plates and prototypes. Roll forming for shelving uprights and rack posts — a different process that STON does not supply, and one you will keep buying in. Most furniture factories end up with a bender plus a folding machine, and one press brake for the rest.
    Can the cell run unattended on a night shift?
    Yes, with automatic loading and stacking. STON panel benders keep a native automatic loading and unloading interface and can be matched with most robotic arm and gantry brands on the market, alongside STON's own truss system and Bronte robotic arm. Fully enclosed rear fencing and laser guarding are specified at order stage for unattended running.
    ما هي إمدادات الطاقة والهواء المطلوبة؟
    Panel benders and folding machines require three-phase 380 V power and 0.6 MPa compressed air. Turret punch presses require 380 V ±5% and 0.55 MPa air, with combined power consumption around 3–5 kW for servo models. Voltage and frequency are configured for the destination country before shipment.
    هل يمكن توريد الآلات إلى تركيا أو المكسيك أو روسيا أو جنوب شرق آسيا؟
    Yes — these are among STON CNC's main export markets. Supply voltage and frequency are configured to the destination before shipment, CNC and HMI language can be localised, and machines carry CE marking under Directive 2006/42/EC where required. Export documentation, packing and container loading are handled in-house in Qingdao, one hour from major export ports and the airport.
    كيف يتم التعامل مع قطع الغيار والصيانة خارج الصين؟
    تلتزم شركة STON CNC بالاستجابة في غضون ساعة واحدة وحل المشكلات في الموقع خلال 48 ساعة في جميع أسواق التصدير التي تزيد عن 80 سوقًا، مدعومة بدعم فني عن بُعد على مدار 7×24، ومستودع مخصص لقطع الغيار، وترقيات برمجية مجانية طوال عمر الماكينة. يتم تقديم عرض أسعار لمجموعة قطع الغيار الموصى بها مع الماكينة، بحيث تكون قطع الغيار المعرضة للتآكل الشائع متوفرة في مخزونكم الخاص بدلاً من شحنها جواً في منتصف نوبة العمل.
    هل تقدمون وثائق شهادة المطابقة (CE) للتصدير إلى أوروبا؟
    STON machines are CE certified and the company holds ISO quality certification. Technical documentation for the Machinery Directive is prepared with each EU shipment, and safety configuration — laser guarding, fully enclosed rear fencing, protective covers on moving parts — is specified at order stage.
    How do we confirm our parts can be made before committing?
    Send part drawings with material, thickness and monthly volume, and include your smallest drawer component. Our pre-sales engineers review the drawings and provide free sample parts to validate feasibility, optimise the bend program and tooling, and shorten ramp-up after installation.

    تم التحقق من صحة المواصفات الواردة في هذه الصفحة مقارنةً بالوثائق الهندسية الخاصة بشركة STON في 4 أغسطس 2026. ويتم التأكد من حدود التشكيل مقارنةً برسوماتكم الخاصة قبل تقديم عرض الأسعار. نُشرت في 4 أغسطس 2026 · آخر تحديث في 4 أغسطس 2026 · تمت مراجعتها بواسطة فيكي شو، رئيسة قسم المبيعات الخارجية.

    الآلات، والأدلة، والتطبيقات ذات الصلة

    يتم تصنيع جميع آلات STON المذكورة في هذه الصفحة في مصنعنا في تشينغداو. قارن بين سلاسل الآلات، واقرأ أدلة الشراء، أو اطلع على كيفية تهيئة نفس المعدات للاستخدام في الصناعات المجاورة.

    الخطوة التالية

    Send us your drawer and door drawings

    We will come back within 24 hours with a machine recommendation, a bend-sequence check on your smallest part, and an honest answer on whether the whole family fits one cell.

    • مراجعة الجدوى من قِبل مهندسي ما قبل البيع، وليس من قِبل مندوب المبيعات
    • عينات مجانية من القطع قبل تقديم الطلب
    • تصميم الخطوط المرسوم وفقًا لمخطط الطابق الفعلي الخاص بك
    • خيارات التهيئة بثلاثة مستويات للإخراج

    هل تفضل التحدث أولاً؟
    واتساب: +86 18153226091
    البريد الإلكتروني: [email protected]

    احصل على اقتراح للتجهيز

    أرسل متطلباتك عبر نموذج الاستفسار الآمن الخاص بنا. سيقوم فريقنا بالرد عليك في غضون 24 ساعة.

    اطلب عرض أسعار مخصصاً
    Drawings can be attached in the reply email. We respond Monday to Saturday.

    احصل على عرض أسعار الآن

    أرسل لنا احتياجاتك - سنعاود الاتصال بك خلال 24 ساعة

    سواء أكنت تقوم بترقية خط إنتاج قائم أو تبدأ مشروعًا جديدًا، فإن STON ستخصص حلاً بنظام التحكم الرقمي للإنتاج الخاص بك.