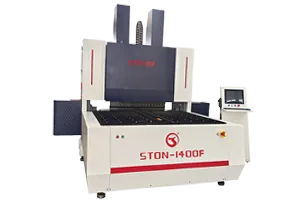
نحن مسؤولون عن البناء-----نحن مسؤولون عن التصنيع-----نحن مسؤولون عن التدريب

A press arm panel bender is worth evaluating when a blank offers a usable mechanical clamping area but limited space for vacuum sealing. A suction cup panel bender is worth evaluating when the blank provides suitable sealing areas for stable vacuum handling. Neither choice can be confirmed from material thickness alone: gripping access, holes, surface condition and clearance throughout the bend sequence must also be checked.
For electrical enclosures, ventilation panels, metal furniture and other formed sheet metal parts, the practical question is whether the selected system can control the workpiece from its first loading position to its finished shape.
1. What Is the Difference Between Press Arm and Suction Cup Panel Benders?
In this comparison, “press arm” and “suction cup” describe how the workpiece is gripped and manipulated. They do not mean that one machine uses an arm to make the bend while the other bends with vacuum.
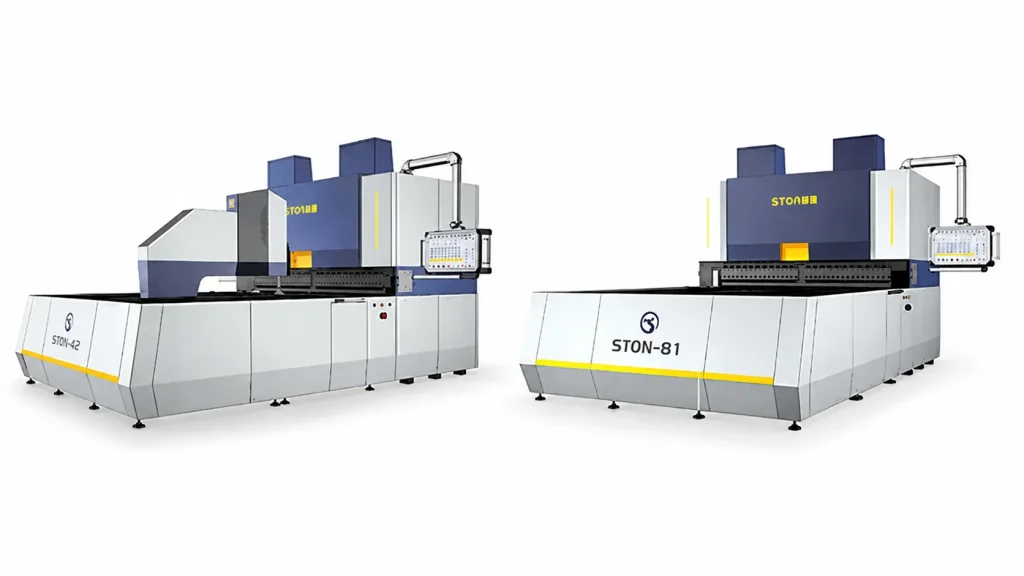
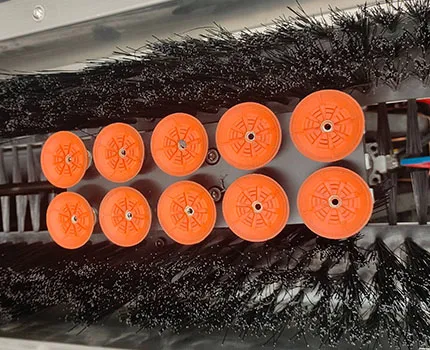
A press arm arrangement uses mechanical contact to hold and position the blank. A suction cup arrangement uses vacuum gripping for workpiece handling. The bending tools and hold-down arrangement still perform their respective forming functions. shen-chong.com
Use the following table as an initial screening framework, rather than approval for a particular STON model.
| عامل الاختيار | Press Arm Panel Bender | آلة ثني الألواح المزودة بكؤوس شفط |
| Gripping area | Needs an accessible, sufficiently supported clamping location | Needs suitable sealing areas for the installed cups |
| Holes and cut-outs | Can be considered when holes leave usable clamping locations | Cup positions must avoid leakage paths or use a validated gripping solution |
| Surface condition | Assess contact pressure, friction and acceptable marks | Assess sealing, friction, cup material and surface compatibility |
| Formed geometry | Check arm, clamp and tooling clearance throughout the sequence | Check cup access and clearance as walls and flanges develop |
| Small or narrow parts | Confirm clamping access and the model’s forming limits | Confirm cup footprint, support and the model’s forming limits |
| Automation | Confirm loading, transfer and unloading separately | Confirm loading, transfer and unloading separately |
Holding the flat blank successfully is only the first check. Ask how the machine maintains control after each bend.
A perforated sheet does not automatically require a press arm panel bender. Its suitability for vacuum handling depends partly on where the openings fall relative to the suction cups.
A ventilation panel with a solid border or central strip may provide usable sealing zones. A different panel with openings across every available contact area may be difficult to hold with the proposed cup arrangement.
بالنسبة لـ press arm system, identify where the clamp will contact the sheet. That location must have sufficient support and remain accessible during the required movements. Mechanical gripping does not remove collision or deformation risks. Manufacturers describe press-arm feeding configurations for perforated and embossed sheets, but suitability remains specific to the equipment and part. SENFENG
Ask the supplier to mark the proposed gripping locations on the actual blank drawing and check them against the complete forming sequence. Hole density alone is not a sufficient selection rule.
Yes. Provide the supplier with the surface condition that will actually enter production.
For vacuum handling, cup shape and material affect how the system adapts to the contact surface. Specialised suction cups can handle some oily or uneven sheets, so oil is not an automatic reason to reject vacuum handling. Equally, that capability cannot be assumed for every installed cup. schmalz.com
For mechanical clamping, review the contact area and whether its appearance remains acceptable after processing.
| Surface Condition | What to Confirm |
|---|---|
| Brushed stainless steel | Whether contact marks are acceptable on the visible face |
| Pre-painted sheet | Whether gripping, table support and tooling preserve the coating |
| Protective film | Whether the actual film seals, slips, lifts or leaves marks during handling |
| Oily sheet | Whether the proposed contact system maintains grip during movement |
| Embossed or uneven sheet | Whether the available contact zones suit the selected gripper |
Request a sample test using the same finish, film and preparation as production. Neither handling method alone guarantees a scratch-free finished part.
Check the flat blank and the finished part together. Maximum bending length is only one part of the selection.
Your review should include:
– Material grade, thickness and relevant strength information.
– Blank length, width, weight and support requirements.
– Minimum part size and usable gripping area.
– Flange heights, return bends, hems and corner geometry.
– Tool, manipulator and machine clearances.
– Finished-part release and removal.
A blank may fit on the table but become difficult to rotate or remove as its walls develop. Similarly, a small component may fit within the maximum capacity while falling below the machine’s practical gripping or forming limits.
Press arm handling does not, by itself, establish a higher bending-thickness capacity. Confirm capacity for the selected model, frame, material and bend length in the written proposal.
The examples below illustrate a review method. They are not customer case studies or confirmed processing results.
| Illustrative Part | Initial Review Direction | Essential Check Before Selection |
|---|---|---|
| Cabinet door with a broad, uninterrupted centre | Evaluate suction cup handling; compare press arm handling if appropriate | Sealing or clamping access, surface marks and return-flange clearance |
| Ventilation panel with dense perforations | Evaluate mechanical gripping and any remaining vacuum sealing zones | Whether usable contact areas remain throughout the sequence |
| Pre-painted enclosure panel | Evaluate both methods with the actual finish | Appearance after gripping, table movement, bending and unloading |
| Small tray with tall walls | Start with minimum forming size and collision review | Gripper access, corner tooling, wall clearance and finished-part removal |
For each part, the output should be a feasible configuration and bend sequence. A recommendation based only on “cabinet,” “HVAC” or “furniture” is too broad.

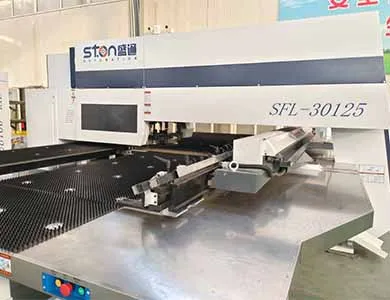
STON lists a press arm CNC panel bender range and an A1/B1 suction cup CNC panel bender range, with automation options described on their product pages. ستون
Distinguish the external loader from the machine’s internal workpiece manipulator. A vacuum loader picking a sheet from a stack does not, by itself, make the bending machine a suction cup type.
When reviewing automatic loading and unloading systems, ask how sheets are separated, located, transferred and released. Check the finished-part stacking method as carefully as the blank pickup.
Confirm the quoted scope: an automation interface, an optional loader and a complete commissioned cell are different deliverables.
Compare the two configurations on the same representative parts and production assumptions.
A useful demonstration includes loading, locating, repositioning, all bends and unloading. For mixed batches, also account for program preparation and changes to tooling or gripping setup.
A quoted time for one bending action does not establish output per hour. Likewise, a lower machine price may not represent lower cost per accepted part.
Ask for an itemised proposal covering the machine, tooling, gripping equipment, automation, installation, training and recommended maintenance items. Then compare:
– Accepted parts produced during the same test period.
– Required operator tasks.
– Changeover work between representative parts.
– Surface quality and dimensional results.
– Maintenance and consumable requirements.
There is no reliable universal rule that press arm machines are always more accurate, or that suction cup machines are always faster or cheaper.
Start with representative production drawings, including difficult parts and frequent changeovers.
| معلومات | لماذا هذا مهم؟ |
|---|---|
| Flat blank and finished-part drawings | Identifies contact zones, bend geometry and clearance questions |
| Material grade and thickness | Establishes the basis for capacity review |
| Surface finish and protective film | Supports gripping and appearance assessment |
| Hole patterns, cut-outs and embossed features | Reveals potential sealing and clamping restrictions |
| Monthly quantities, batch sizes and part mix | Helps assess setup frequency and automation scope |
| Workshop layout and handling requirements | Supports loading, unloading and cell-layout planning |
| Dimensional and cosmetic acceptance criteria | Gives the sample test a clear pass-or-fail basis |
Explore STON’s CNC panel bender machines و contact the STON team with your drawings to discuss a suitable configuration.
Before ordering, request confirmation of the proposed gripping method, tooling, bend sequence, automation scope and representative sample results.
Can a suction cup panel bender process sheets with holes?
Potentially. The proposed cup layout needs suitable sealing areas, or another validated solution for the openings. Check the actual blank and handling sequence rather than rejecting or approving
it based only on the presence of holes.
Is a press arm panel bender always better for perforated panels?
No. Mechanical gripping is worth evaluating when vacuum sealing is restricted, but the blank must still provide accessible, supported clamping locations and sufficient clearance.
Will suction cups prevent scratches on pre-painted panels?
Not automatically. Cup compatibility, cleanliness, table contact, tooling and unloading all affect appearance. Test the actual production finish against agreed cosmetic criteria.
Can both types be integrated into an automated bending cell?
Both STON product ranges describe automation options. The particular loader, gripper, controls and unloading arrangement must be confirmed for the quoted configuration.
Should I choose by sheet thickness or gripping method first?
Check both. The machine must meet the forming requirements and maintain control of the workpiece. Passing one check does not compensate for failing the other.
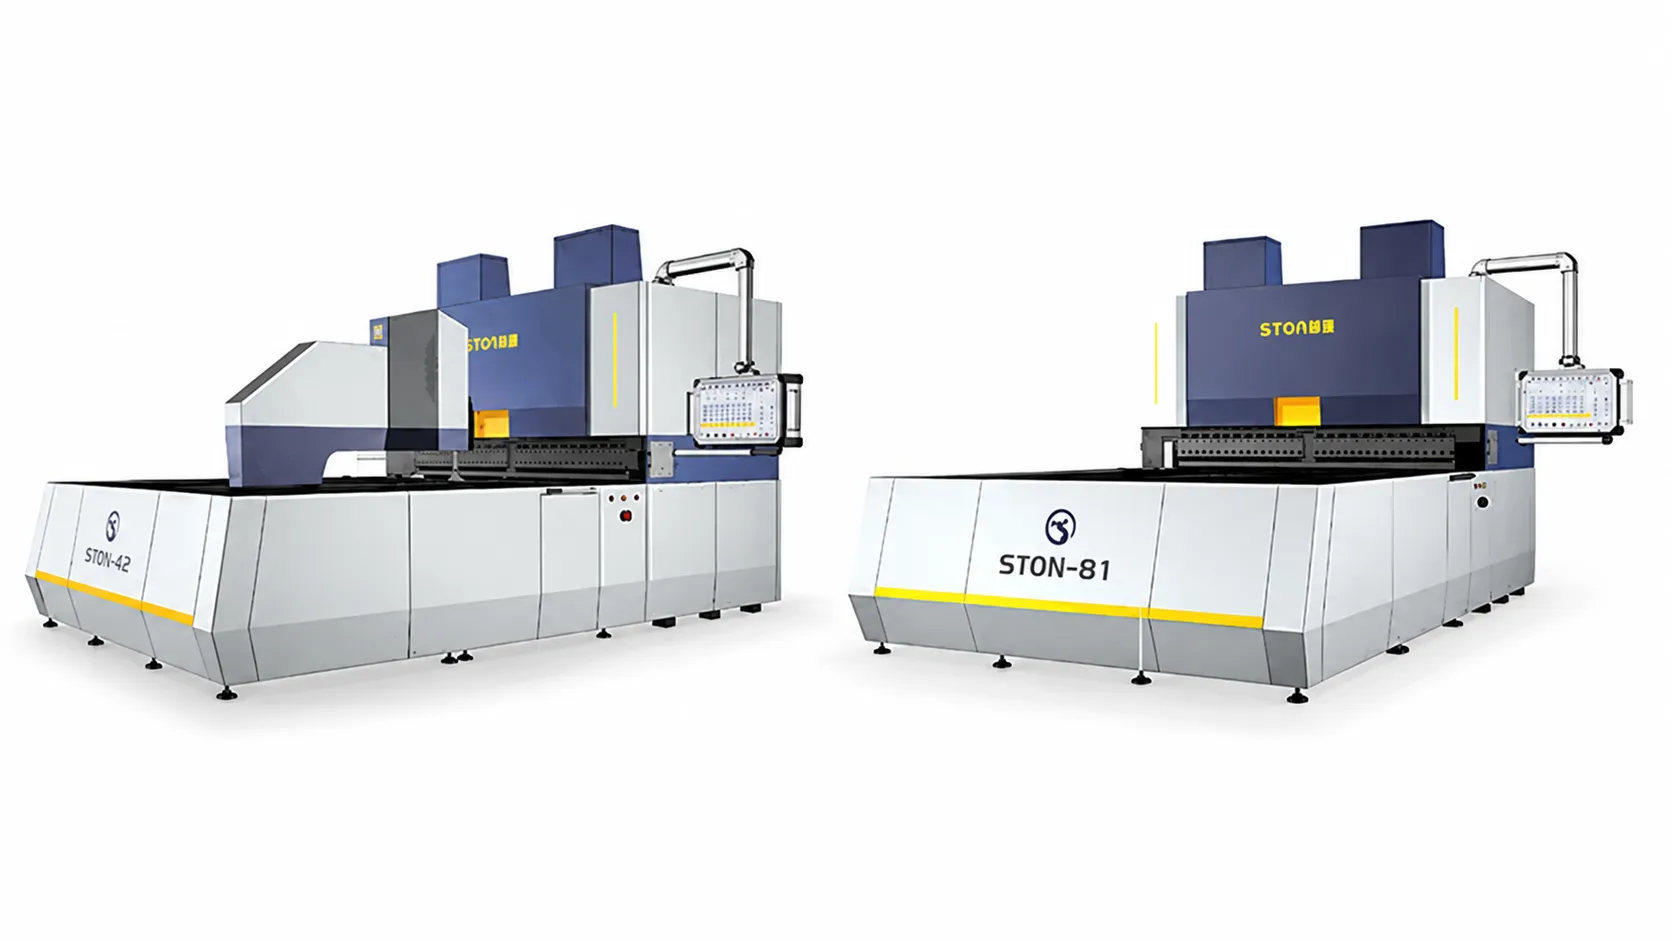
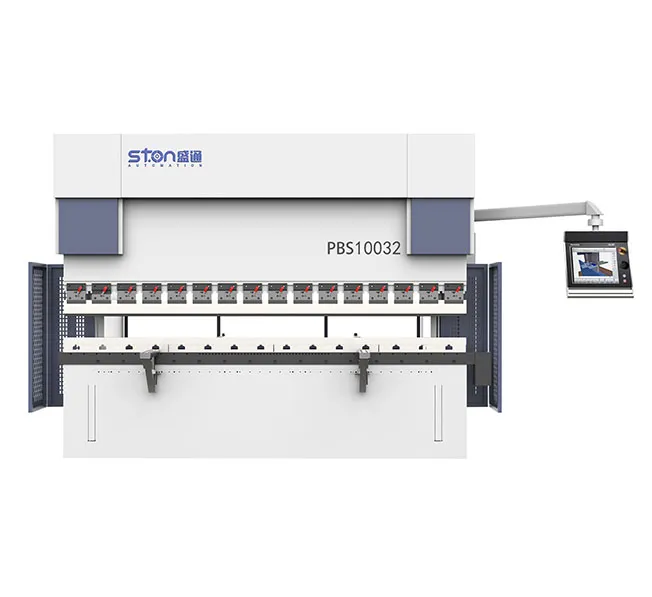
سواء أكنت تقوم بترقية خط إنتاج قائم أو تبدأ مشروعًا جديدًا، فإن STON ستخصص حلاً بنظام التحكم الرقمي للإنتاج الخاص بك.